Highlighting the thinkers and their ideas driving the evolution of Offsite Construction. 
Be inspired, be informed, be innovative!

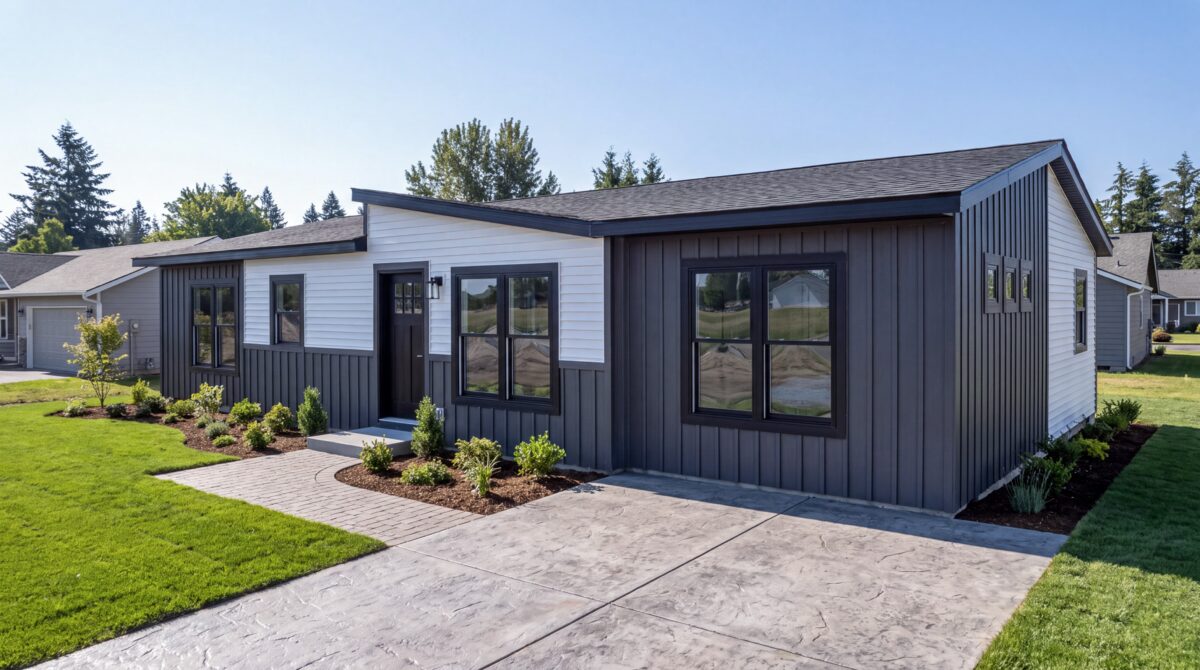
Cavco Takes Away the Chassis—and Gives Factory-Built Housing Something to Think About

The Grande Arbor pairs a new construction approach with a floor plan built around the realities of families sharing a home.

I have spent enough years watching factory-built housing evolve to know that the most interesting changes aren’t always the ones you notice walking through the front door. Sometimes, the development worth paying attention to is underneath the house. In Cavco’s latest announcement, it is something that will no longer be there.

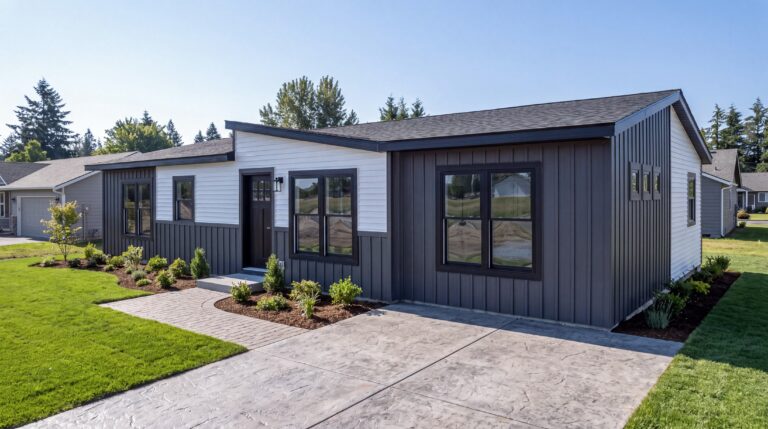
Cavco says it will debut the first HUD-code manufactured home constructed without a permanent steel chassis at the 2026 Innovative Housing Showcase, September 22–24 on the National Mall in Washington, D.C. Called the Grande Arbor, the home combines that construction change with two primary suites designed for multigenerational living. Cavco also describes it as its first HUD-approved frameless manufactured home in its company announcement.

That combination caught my attention. A different way to build the home is interesting to our industry, but a different way for a family to live comfortably together may be what gets a buyer to sit down and discuss purchasing one. The Grande Arbor brings both conversations into one home.For people outside our industry, a permanent steel chassis probably doesn’t come up very often around the dinner table. Buyers are more likely to ask what the home costs, how it looks on their property, and whether everyone will have enough room. Yet decisions made underneath the floor can influence the answers to several of those questions.

According to Cavco’s announcement, eliminating the permanent chassis allows a lower-profile installation and creates additional design flexibility. Think about the relationship between the front door, the yard, the sidewalk, and the neighboring houses. Those details help determine how naturally a new home fits into an established street, even when viewers know nothing about its construction.

I would expect builders considering infill lots and neighborhood developments to study that closely. A house can look attractive in a photograph and still require considerable work to fit a particular property. A lower installation profile offers another option to explore, although foundation design, grading, drainage, and site details still have to work together.

There is also a practical distinction worth keeping clear. “Frameless” refers to a home without the permanent steel chassis; the home still needs an engineered structural system. It also needs a workable way to get from the factory to its foundation. Those are precisely the details production managers, transporters, and installation crews will want to understand.

That is where my questions begin. How will the home be supported during transportation? What equipment and procedures will the installation require? How will the factory coordinate with the foundation contractor, and what will the complete installed package cost? The announcement introduces the product, but those answers will help determine how broadly the approach can be used.

I would be careful about assuming that removing a major component automatically produces an equivalent reduction in the buyer’s final bill. Costs have to be evaluated across the whole job, including production, transportation, foundation work, installation, and finishing. Anyone who has watched a seemingly inexpensive house become an expensive completed project understands why that distinction matters.

The commercial opportunity is nevertheless interesting. Cavco is describing a product that could give builders more flexibility in how they present and place manufactured housing. Whether that opportunity becomes a repeatable business will depend on the finished result, the delivery process, and the economics of each project.

Inside the Grande Arbor, the company is addressing another practical challenge: how to put more than one generation under the same roof without making everyone feel as though they are living in someone else’s space. Its double grande suite layout places primary suites at opposite ends of the house, with a shared kitchen, dining area, and living space between them.

I think that arrangement deserves as much attention as the missing chassis. There is a meaningful difference between offering an adult family member a spare bedroom and designing the house from the beginning to accommodate two adult households. Privacy becomes part of the plan, not something everyone tries to negotiate after moving day.

Consider parents sharing a home with an adult child, or a family welcoming an older parent. They may enjoy meals together and appreciate being close enough to help one another, while still wanting different bedtimes, different television programs, and a door they can close. A successful floor plan has to make room for those ordinary details.

Sharing a home also involves more than dividing expenses. It can mean coordinating work schedules, caregiving, visitors, storage, and daily routines. Two well-separated suites cannot resolve every family disagreement, but the arrangement can give people a better starting point than a floor plan that treats one household as permanent guests.

For builders and sales teams, that changes the conversation. Instead of simply counting bedrooms, they can ask how the buyers expect to use the house over time. Who needs privacy now? Who might join the household later? Which shared spaces will see the most activity? Those questions can reveal whether a home actually fits the family purchasing it.

Cavco will exhibit the Grande Arbor with UMH Properties, and its Rocky Mount, Virginia, team built the display home. That same operation also introduced the Anthem in 2023, which the announcement described as the first nationally available HUD-approved manufactured duplex. Together, the projects show the company exploring different ways to accommodate households through factory production.

For the broader offsite industry, I see a useful business question here: how quickly can a new product move from an impressive display to a dependable offering? A showcase home attracts attention, but the repeat orders depend on clear specifications, reliable delivery, capable installation partners, and a price buyers can understand.

The modular side of the industry will have reasons to watch, too. Builders compare available products against a project’s needs, and additional choices can change those comparisons. The practical discussion will center on design flexibility, site compatibility, schedules, and total cost—the same questions that eventually reach every factory’s sales desk.

What interests me most about the Grande Arbor is that Cavco has paired a construction development with a recognizable household need. The engineering gives the industry something to examine, while the floor plan gives families something they can picture themselves using. Both have to work for the product to find a lasting market.

I will be watching what happens after the National Mall display comes down. Show me the completed neighborhood installation, the builder’s experience, the total project cost, and the family settling into those two suites. That is where we will learn how much this new approach changes the everyday business of delivering a home.
When an OSB Mill Idles, What Is It Telling Home Factories?

Most people in offsite construction will never visit an oriented strand board mill. We see the finished sheets arriving at a modular plant or panel shop, ready to become floors, walls, and roofs. We know what a late delivery can do to a production schedule, and we know what a price increase can do to a quote. It is easy, though, to pay less attention when a mill announces that it will stop making those sheets.

LP Building Solutions has given us a reason to pay attention. On September 1, the company announced that it will indefinitely curtail OSB production at its Jasper, Texas, facility beginning in October. The mill has annual production capacity of approximately 475 million square feet, measured on a 3/8-inch basis. LP cited soft demand and said it had reviewed operating costs, capital requirements, logistics and long-term asset utilization across its manufacturing network. LP’s announcement

Preview in new tab

The word indefinitely matters. LP has left open the possibility of restarting production when conditions warrant it, but it has given no restart date. In a September 1 SEC filing, the company estimated $4 million to $6 million in severance and other one-time costs associated with the curtailment.

Those figures reflect a human cost. Citing a Texas workforce notice, Chron reported that about 150 jobs are affected, with cuts expected to take effect November 1. LP says it will provide career-transition assistance and help employees apply for openings at other company facilities. For the people in Jasper, the industry’s discussion of capacity and demand is immediately personal.

Confidence surveys tell us what builders think may happen. A decision to idle a large operating mill tells us what one major supplier is prepared to do with its capacity today. LP is responding to conditions in the OSB market, and its announcement should be read as such. It does not prove that every housing market is weakening equally, or that every modular factory’s orders are falling.

It does tell us that LP sees insufficient demand to justify keeping Jasper in production under current conditions.

That distinction matters to anyone building with wood panels. OSB is a basic input in much of residential construction, including panelized systems, modular homes and manufactured housing. A company that makes it has to consider more than the price on this week’s orders. It must decide whether expected volume will cover the cost of operating a mill, maintaining its equipment and moving its output to customers.

Offsite factories face a similar calculation, even if their production lines are smaller. We may have a promising list of projects, but how many are approved, financed, engineered, and ready to enter production? How much of the schedule rests on contracts, and how much rests on expectations? Those are different numbers, and a factory that confuses them can stay busy preparing for work that never arrives.

Some builders may look at an OSB curtailment and hope that soft demand will bring material-price relief. If their purchase costs decline, that could help margins on projects already under contract. It could also make a few new projects easier to price. Factory managers should take those opportunities where they find them.

I would still want to know why the price is falling. If suppliers have more board than builders are willing to buy, cheaper sheathing may arrive alongside fewer home orders. Saving money on each sheet does little good if the line lacks enough projects to keep its crews employed and its overhead covered.

Nor should we assume that curtailing one mill guarantees any particular price outcome. Other producers may adjust output, demand may change, and delivered costs vary by location. A factory should update its purchasing forecasts using actual supplier quotes while examining its sales pipeline with equal care. The material price and the strength of the order book belong in the same conversation.

There is another timing problem here. Factories often quote a project long before buying all its materials. A favorable price today may disappear before production begins. Conversely, a factory locked into an older, higher material allowance may have an opportunity to improve its margin. Either result depends on contract terms, purchasing discipline and when the work actually reaches the line.

The most useful part of LP’s announcement may be its description of the decision process. The company says it considered operating costs, capital requirements, logistics, and long-term utilization. I would put those four subjects on the agenda of any offsite manufacturer considering a new line, another shift or a plant expansion.

Operating costs: What does it cost to run the facility at the volume we can reasonably expect, rather than at the volume shown in an expansion presentation? A factory can achieve an impressive weekly output during its busiest month and still struggle over the full year.

Capital requirements: What equipment, repairs, or building improvements will the plant need to remain productive? Delaying maintenance can make this year’s numbers look better while leaving next year’s management team with an expensive problem.

Logistics: Can we deliver profitably to the markets where our customers are buying? For modular manufacturers, transportation, carriers, crane scheduling, and site readiness can determine whether apparent factory efficiency survives beyond the loading door.

Long-term utilization: How much dependable work will keep the operation healthy through a full cycle? A factory designed for peak demand still has to pay its bills when orders return to ordinary levels.

LP’s answers led it to curtail a mill. Another company answering the same questions may decide to invest, change its product mix or move work between facilities. The management lesson is to ask before circumstances make the choice for you.

Our industry spends considerable energy announcing what factories can produce. We hear about homes per day, modules per week, and square feet of new production space. Those figures describe capability. They do not tell us how many customers have signed, how many projects have cleared permitting, or how many job sites will be ready to receive what the factory builds.

That gap matters most in offsite construction. A mill may be able to sell a standard panel into a broad distribution network. A modular factory often needs the right project, drawings, approvals, financing, builder, and installation schedule to come together before its capacity becomes revenue. When one piece slips, the factory may be left with idle stations—or finished modules occupying its yard and carriers.

This is why I would rather hear a factory manager discuss production-ready backlog, contribution margin, and delivery performance than theoretical maximum output. Capacity matters, but its value depends on how consistently the whole business can use it.

I do not see LP’s Jasper decision as a prediction that offsite construction has reached some permanent limit. Markets move, and LP has said it may restart curtailed capacity when conditions support doing so. I see the decision as a reminder that experienced manufacturers sometimes need to reduce output to protect the business through a difficult part of the cycle.

The people losing work in Jasper deserve more than a passing mention in an industry discussion about OSB prices. Their situation also gives factory leaders a reason to examine their own plans honestly. If demand is softening, the responsible time to review costs, capital needs, logistics, and backlog is while management still has choices.

LP has done that review and made a difficult decision. Every modular, manufactured and panelized housing company should be asking what the same review would reveal inside its own factory.

Humanoid Robots Are About to Enter the Modular Housing Factory

For years, the offsite construction industry has talked about automation as though every factory would eventually resemble an automobile plant. Robots would frame walls, install windows, apply adhesives, move materials, and complete repetitive tasks while a smaller number of highly trained employees monitored the production line.

That vision has proven far more difficult to achieve in homebuilding than many technology companies expected. Houses contain flexible materials, constantly changing components, tight spaces, and dozens of tasks requiring people to see, feel, and adjust what they are working with. Traditional industrial robots perform extremely well when every component arrives in precisely the same position, but construction materials do not always cooperate.

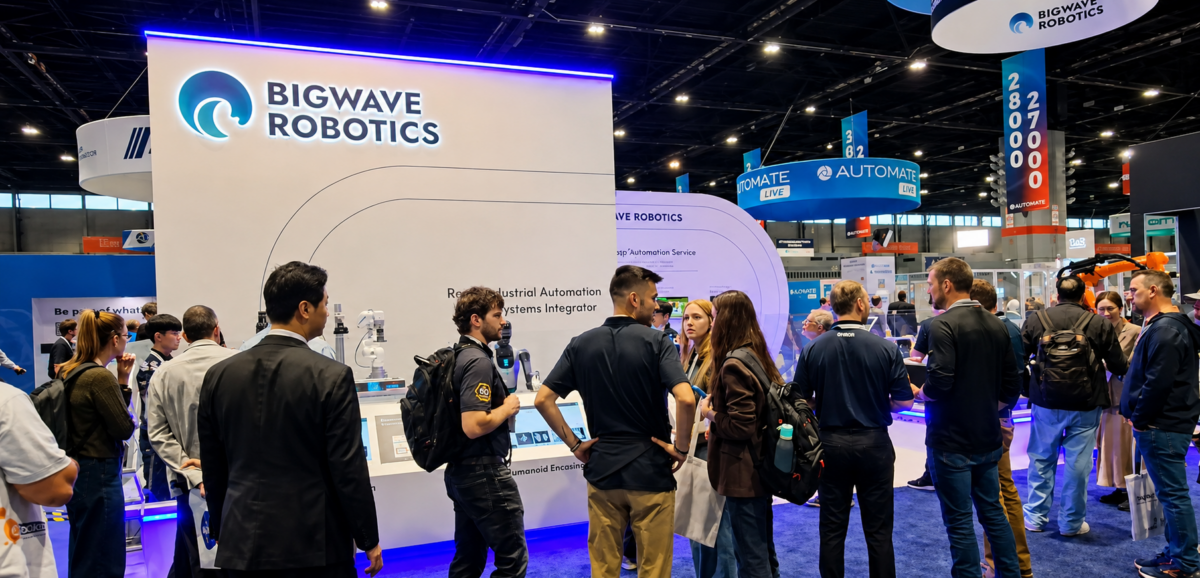
Bigwave Robotics believes humanoid robots may close some of that gap.

The robotics company has announced an agreement with Space Manufacturing Lab, described as the country’s largest modular housing producer, to begin introducing humanoid robots into factory production and onsite installation. The first assignment will not be framing walls, hanging drywall or carrying modules. The robots will begin with one of the least pleasant jobs in residential construction: installing fiberglass insulation.

Insulation installation may seem like a modest starting point for a humanoid robot, but it makes a lot of sense. Fiberglass can irritate workers’ skin, eyes, and respiratory systems, especially when they don’t follow proper protective equipment and ventilation procedures.

Many factories also find this task difficult to staff consistently. Employees must lift, position, cut and fit insulation into cavities while working around wiring, plumbing, framing irregularities and other obstructions. The work is repetitive, physically uncomfortable, and not the type of job most employees hope to perform for the rest of their careers.

Unfortunately, it is also difficult to automate with conventional industrial equipment. Fiberglass insulation is flexible, compressible, and irregular. It bends, folds, and changes shape when handled, making it very different from the metal parts and rigid components that robots have traditionally moved through manufacturing plants.

A fixed industrial robot performs best when the material, workstation and required movement remain virtually identical during every cycle. Insulation does not always provide that level of predictability. A humanoid robot equipped with vision systems, sensors and artificial intelligence may be able to recognize the cavity, adjust its movements and manipulate the material in ways that more closely resemble a human worker.

That is the theory. Space Manufacturing Lab and Bigwave Robotics now have to prove it works under real production conditions.

Space Manufacturing Lab already uses factory prefabrication and standardized production methods to manufacture wood modular housing. Rather than replacing its entire production system, the company plans to introduce humanoids gradually alongside its existing automated equipment and human workforce.

That approach may matter more than the robots themselves.

Factories often make the mistake of treating automation as an all-or-nothing decision. Management becomes attracted to the idea of building a highly automated plant and begins purchasing expensive equipment before determining whether the product, production volume, and processes justify the investment.

A more practical strategy is to identify a specific task that is dangerous, repetitive, difficult to staff or responsible for a production bottleneck. The factory can introduce automation at that point, measure the results, and expand only after the technology proves it can improve safety, quality, output, or cost.

Insulation gives the companies a clearly defined place to begin. Bigwave Robotics says it will use what it learns from that application to identify other factory and installation tasks that humanoids may eventually perform.

The important word is “eventually.” Introducing a humanoid robot into a promotional video is relatively easy. Teaching it to work safely and productively during an eight-hour shift, alongside employees and under changing factory conditions, is an entirely different challenge.

Humanoid robots are sometimes presented as the answer to construction’s labor shortage because they are designed to operate in environments originally built for people. They may be able to walk through a factory, use tools, and perform tasks without redesigning every workstation.

That does not mean a humanoid can solve an undisciplined production process.

If drawings change after production begins, materials arrive late, components are stored in the wrong location, or every house differs significantly from the last, the robot will face many of the same problems that frustrate human workers. Artificial intelligence may help a machine adjust to variations, but it cannot turn a poorly organized factory into a dependable manufacturing operation.

Space Manufacturing Lab appears to understand the importance of standardization. Its modular system is based on completing much of the house in a controlled factory environment, and the company recently introduced the Samsung AI Modular Home in cooperation with Samsung Electronics. That concept combines modular construction with artificial intelligence and Internet-connected home technology.

Adding humanoid robots to the production process represents another step toward connecting the factory, the product, and the technology inside the finished home. Whether customers ultimately care who—or what—installed the insulation will depend upon the results. The finished work must still meet code, perform properly, and be completed at a cost that supports the selling price.

Bigwave Robotics intends to use the information collected at Space Manufacturing Lab’s facilities to develop construction-focused “physical AI” systems. Unlike AI programs that generate reports, drawings, or schedules, physical AI allows machines to perceive their surroundings, make decisions, and perform work in the real world.

The company has also made it clear that its ambitions extend beyond its domestic market. Bigwave Robotics plans to pursue modular housing opportunities in other countries, including North America.

That should catch the attention of U.S. and Canadian modular, manufactured and panelized housing producers. Many North American factories are struggling to recruit and retain production employees, especially for jobs involving repetitive motion, uncomfortable working conditions or physically demanding tasks.

The industry is not likely to replace entire production crews with humanoids anytime soon. The first useful applications will probably involve individual jobs that workers dislike, that contribute to injuries or that repeatedly interrupt production because people cannot be found to perform them.

Insulation, sanding, material handling, fastening, inspection and certain finishing tasks could all become candidates. Onsite work may be harder because weather, uneven terrain, changing conditions, and unpredictable obstacles make construction sites far less controlled than factories.

The robot’s cost is only part of the equation. A factory must also consider programming, integration, maintenance, safety systems, employee training, production interruptions, and the technical personnel required to keep the equipment operating.

Management must measure more than whether the robot can perform the task. It must determine whether the machine can complete the work at the required speed, maintain consistent quality, and operate often enough to justify the total investment.

If a humanoid robot installs insulation twice as slowly as an experienced employee and requires frequent human assistance, it may be an impressive technical demonstration without being a sound manufacturing investment. If it can work consistently, reduce employee exposure, improve installation quality and relieve a chronic labor shortage, it could become extremely valuable.

The factory should know the difference before ordering a fleet.

Humanoid robots will almost certainly become part of offsite construction, but their arrival will not eliminate the need for good factory management. In fact, they may expose weak management more quickly because automation depends upon standardized products, reliable material flow, complete information, and repeatable processes.

Space Manufacturing Lab and Bigwave Robotics are beginning in the right place. They have selected a specific task that is unpleasant for employees and difficult for conventional robots. If the humanoid can install insulation safely, accurately, and economically, the companies will have demonstrated something far more useful than a robot walking across a factory floor for the cameras.

The real opportunity is not replacing every employee. It is allowing people to move away from the dirtiest, most dangerous, and least desirable jobs while machines perform the work that factories consistently struggle to staff.

Humanoid robots may be coming to modular housing, but the winners will not be the factories that purchase them first. They will be the factories that know exactly why they need them, where they should use them, and how the investment will improve the home coming off the line.

Everybody Has a Dream. Offsite Construction Demands More.

Everybody dreams of doing something different from what they do today. Everybody.

Some dream about starting a business, inventing a better product or solving a problem everyone else has learned to tolerate. In offsite construction, those dreams often begin with a belief that there must be a faster, better, and more affordable way to build.

The housing shortage is real. Skilled labor is becoming harder to find. Traditional construction remains slow and expensive. From the outside, offsite construction looks like an industry waiting for someone with a fresh idea to come along and change everything.

That is what makes it so attractive to dreamers. It is also what makes it so dangerous.

Dreaming is emotionally safe. Pursuing the dream requires money, experience, discipline, and the willingness to hear things we may not want to hear. An untested dream can remain perfect forever. Once it becomes a business, reality begins asking some very difficult questions.

I was reminded of that recently during conversations with several people who believe they have ideas that could change offsite construction.

The first group has moved beyond simply talking about its idea. They have developed a product, assembled a plan, and are preparing to launch.

After learning what they are doing, I have a great deal of confidence that their product will be adopted by the industry. That confidence does not come from their enthusiasm alone. I have met many enthusiastic people whose companies disappeared before producing anything.

My confidence comes from the fact that their idea appears to address an actual industry problem. The people involved understand the market, recognize the obstacles ahead, and have thought about how the product will move from concept to adoption.

There are never any guarantees, especially in construction. However, this group seems to understand that inventing something is only the beginning. The real challenge is convincing factories, builders, developers, and other industry professionals to change what they are already doing.

That requires more than a dream. It requires a practical path into the market.

The second conversation was with someone preparing to build a company around another offsite construction idea. They told me they were working with a consultant to raise the capital needed to get started.

That sounded encouraging until I asked a simple question.

Does the consultant have hands-on experience in construction—and specifically in offsite construction?

They said the question had never come up. The consultant’s job was to bring in the money.

That answer concerned me.

Raising capital matters, but money does not fix a flawed production plan. It does not automatically create customers, establish realistic pricing, navigate building codes, manage transportation or coordinate site completion. Money simply lets a company start spending money.

If the people advising the founders do not understand construction, they may not know which questions to ask before approaching investors. If they do not understand offsite production, they may not recognize how engineering, approvals, factory operations, logistics and fieldwork affect one another.

Investors may fund the factory, machinery and initial payroll while nobody has adequately budgeted for prototypes, design changes, delayed approvals, employee training, warranty work or the long road from an interested prospect to a signed purchase order.

The greatest danger is not always failing to raise enough capital. Sometimes it is raising enough money to build the wrong company.

An experienced capital consultant may be excellent at preparing presentations and introducing investors. That expertise has value. But someone at the table must also understand what happens after the check arrives.

The third conversation involved a young person with a noble goal. He wants to create housing for people living in tents, cardboard shelters, abandoned recreational vehicles, and doorways.

It is hard to criticize that dream. Our country desperately needs better answers for people without safe and permanent housing.

He wanted me to help finance his idea and get it off the ground. He also expected me to provide that help without being paid. When I declined, he got upset because I wouldn’t help him fulfill his dream.

That reaction revealed a problem found in many startups, even when their missions are admirable.

The dream belongs to the dreamer. Other people are not automatically responsible for financing it, validating it or donating their professional experience to make it happen.

Experienced advisors have spent decades learning what works, what fails and what can destroy an otherwise promising company. Asking for a brief opinion is one thing. Expecting someone to help develop, finance and launch a business without compensation is something entirely different.

A noble mission does not eliminate the need for a viable business model. Housing people experiencing homelessness involves land, zoning, utilities, building codes, operating expenses, social services, maintenance and ongoing management. Someone must pay for it all.

Compassion may inspire the idea, but compassion alone cannot sustain the operation.

Most offsite construction dreams don’t fail because founders lack passion. Many fail because they mistake passion for preparation.

Founders often fall in love with the factory, product, panel, module or technology before determining who will consistently purchase it. They see the national housing shortage and assume that demand will naturally find them.

But housing demand is not the same as factory backlog.

People may praise an idea without placing an order. Developers may express interest without controlling a site. Municipal officials may support affordable housing until a specific project reaches the approval process. Investors may like the presentation without understanding how long it will take the company to generate predictable revenue.

Then the factory opens and reality takes over.

Customers request changes. Designs require additional engineering. Approvals take longer than expected. Materials arrive late. Production requires more labor than projected. Transportation becomes complicated, and site work consumes time and money that were never included in the original estimate.

At that point, the founder discovers that a good product is only one part of a complicated system.

Automation will not correct bad estimating. A beautiful factory will not create qualified buyers. Investor money will not replace experienced management. A noble purpose will not pay vendors, employees or insurance premiums.

The first two years reveal the difference between believing in an idea and building an organization that can survive after the initial excitement fades.

Before asking how much money is needed, founders should ask whether the product solves a problem customers will pay to solve. Before selecting equipment, they should understand the production process, available workforce, and realistic sales volume.

Before hiring someone to raise capital, they should make sure someone on the advisory team has worked in construction and understands offsite operations. Before asking others to donate their time, they should recognize the value of the experience they are requesting.

Most importantly, founders must be willing to let knowledgeable people challenge the dream. Advice that exposes a weakness is not an attack on the idea. It may be the very thing that keeps the company alive.

The people who change an industry are not necessarily the ones with the biggest dreams. They are the ones willing to turn those dreams into plans, test their assumptions and listen when experienced people tell them where the dangers are hiding.

A dream can begin with one person, but building a successful offsite company requires customers, capital, knowledge, leadership and a team that understands what happens after the doors open.

The most important question is not, “How good is my idea?”

It is, “Am I prepared to do everything this idea will require when the excitement is gone, the money is being spent, and the industry has not yet said yes?”

Who Should an Offsite Factory Be Consistent For?

An interesting thing happened to me recently while I was thinking about the podcasts I listen to every night.

I have several favorites, but they only release new episodes intermittently. Sometimes I find a new episode waiting for me; other times, I check and discover nothing has been posted. I never know when the next one will appear, and quite honestly, it drives me crazy.

That experience helped me understand something about my own publishing schedule.

I post at least two articles almost every day. Some people may wonder why I feel the need to publish that frequently, especially after writing more than 10,000 articles over the years. The answer is that I want my readers to know they can depend on me to provide something new.

They may not read every article, and I certainly do not expect every topic to interest every reader. But when they visit one of my blogs or look through their LinkedIn feed, I want them to know I will probably have something new for them.

My podcast frustration reminded me that consistency is not simply about producing content. It is about respecting the people who have made your work part of their routine.

That led me to another question: Who should an offsite construction factory be consistent for?

The simple answer is everyone who depends on it.

Factory employees need to know what management expects. They need dependable schedules, clear instructions, proper training, accurate information, and, most importantly, consistent pay.

One of the fastest ways to damage a workforce is to change priorities every few days. A factory may announce that quality is its highest priority on Monday, demand faster production on Tuesday, and then blame workers for defects on Friday.

Employees quickly recognize when management’s words and actions don’t match.

Consistency does not mean conditions never change. Production schedules shift, customers revise projects, materials arrive late, and unexpected problems occur. Employees understand that. What they need is honest communication about what changed, why it changed and what management expects them to do next.

Workers who trust management are far more likely to help the company through a difficult period. Workers who are constantly surprised, blamed, or left uninformed will eventually stop caring—or leave.

Builders and developers don’t buy modules simply because they like the idea of offsite construction. They use a factory because they believe it will make their projects more predictable.

They expect consistent pricing, engineering, production quality, scheduling, communication and delivery.

Unfortunately, some factories sell predictability but operate unpredictably. They promise production dates before engineering is complete, provide pricing that later changes substantially and tell customers that modules will arrive when the factory has not yet secured all the required materials.

Customers can usually tolerate an occasional problem. Construction is filled with unexpected conditions, and experienced builders understand that nothing goes perfectly.

What customers struggle to tolerate is never knowing what will happen next.

A developer should not have to call five times to learn whether a project has entered production. A builder should not discover at the last minute that the delivery date has moved by three weeks. A customer should not receive different answers depending on which factory employee answers the telephone.

Consistency gives customers the confidence to plan everything else around the factory.

Builders, sales representatives, and business-development teams are often the first people to make promises on behalf of a factory. They need reliable information about what the company can build, what it should build, how much it will cost, and when it can be produced.

Problems begin when the factory has no consistent rules.

One salesperson may tell a customer that almost anything can be customized, while production management is trying to reduce variation. Another may promise a quick delivery because the sales team needs the order, even though the production schedule is already full.

That inconsistency creates bad contracts, unrealistic expectations and conflict between sales and operations.

A factory cannot build trust in the marketplace if its own people are giving different versions of the truth.

Suppliers need accurate forecasts, dependable orders and timely payments. Transportation companies, set crews, crane operators and site contractors need reliable schedules and clear coordination.

When a factory repeatedly changes production dates, the effects travel far beyond its walls.

A delayed module may mean a crane sits idle, a set crew loses a day of work, a site contractor must reschedule labor and a developer begins paying carrying costs on a project that is not moving forward.

Factories sometimes consider these outside companies independent vendors. In reality, they are part of the factory’s delivery system. Their performance affects the customer’s opinion of the entire modular process.

If a factory wants dependable suppliers and subcontractors, it must also be dependable to them.

Offsite construction relies heavily on the confidence of inspectors, approval agencies and code officials. They need accurate drawings, complete documentation and consistent workmanship.

A factory that follows its approved processes only when an inspector is watching does not have a quality-control system. It has a performance prepared for inspection day.

The real test of consistency is whether the same standards are followed on every project, during every shift and at every production station.

Quality cannot depend on which supervisor is working, which customer is visiting or how urgently management wants a module moved off the line.

Lenders and investors need consistent and honest financial reporting. They need to understand the condition of the backlog, the profitability of contracts, the amount of working capital required and the risks facing the business.

A factory cannot show optimistic forecasts when it needs financing and then blame customers, suppliers or the economy when those forecasts fail.

Consistency in financial reporting does not mean every report must contain good news. It means the information must be dependable enough for people to make informed decisions.

Bad news delivered honestly can often be managed. Bad news hidden until it becomes a crisis usually can’t be managed.

An offsite factory must also be consistent in the way it presents itself to the market.

Its website, sales materials, articles, advertising and presentations should clearly explain what it does well. If the company specializes in multifamily projects, its marketing should demonstrate that experience. If it serves builders through a dealer network, its website should make the process easy to understand.

A factory should not market itself as everything to everyone.

When the company’s marketing promises unlimited customization, exceptional speed, the lowest price, and the highest quality at the same time, customers will eventually discover that at least one of those promises is not true.

The strongest factories know what they are equipped to build profitably and consistently. They are also willing to say no to projects that do not fit their production system.

After thinking about my frustration with those unpredictable podcasts, I realized that consistency is really another word for dependability.

People return to a podcast, blog or newsletter because they expect something worthwhile to be there. Builders and developers return to a factory for the same basic reason: They believe it will perform as promised.

A factory cannot advertise speed while repeatedly missing production dates. It cannot promote quality while workmanship varies from one module to another. It cannot promise customization while operating a system that requires standardization. It cannot call itself a partner while avoiding difficult conversations with its customers.

The greatest consistency must always be between what the factory says and what it actually does.

My favorite podcasters probably do not realize that their irregular schedules frustrate loyal listeners like me. They may believe people will simply wait patiently for the next episode.

Some offsite factories may make the same assumption about their customers, employees, suppliers, and business partners. They believe everyone will tolerate another changed schedule, another unanswered question, or another promise that does not quite materialize.

Eventually, however, inconsistency becomes the company’s reputation.

I publish two or more articles a day because I want my readers to know they can depend on me. An offsite factory should want the same thing from everyone who relies on it.

Consistency does not mean never making a mistake. It means people know what to expect, get the truth when something changes, and can trust the factory to keep working to fulfill its promises.

In an industry built around the promise of greater predictability, consistency should not be considered a marketing advantage. It should be the foundation of the entire business.

The Information Habit That Could Keep an Offsite Factory from Falling Behind

Yesterday, I wrote about creating a daily resilience plan to help an offsite factory spot financial and operational problems before they become a crisis. That plan depends on monitoring cash, backlog, receivables, margins, labor efficiency, and other internal warning signs.

But an offsite company can be financially stable today and still be quietly falling behind.

The threats may not appear on its daily dashboard. They may be developing somewhere outside the factory—in a competitor’s sales strategy, a new building system, a developer’s changing expectations, an emerging technology or a management decision made by a company in another part of the country.

That raises another important question: Who is responsible for keeping the company abreast of what is happening beyond its own walls?

For years, I have written about modular and offsite construction, factory management, marketing, sales, innovation, startups, automation, and the decisions that can either strengthen or weaken a company. The more I observe, the more convinced I become that many factories do not suffer from a lack of available information.

They lack time, curiosity, and a process for deciding which information deserves attention.

Most factory owners and managers are extremely busy. Their days are consumed by production schedules, engineering questions, customer changes, employee problems, material shortages, inspections, transportation and cash flow.

They may begin the morning intending to read an industry article, study a competitor’s website or learn about a new manufacturing process. By noon, that intention has disappeared beneath a stack of more immediate problems.

This is understandable. A module sitting unfinished on the production line demands more attention than an article about artificial intelligence, a new panelized system or a factory opening three states away.

The problem is that urgent work can gradually crowd out important learning.

Management may know exactly what happened inside the factory yesterday while remaining almost completely unaware of what is changing in the surrounding industry. When that continues for several years, the company may become very efficient at operating a business model that the market is slowly leaving behind.

Keeping informed means more than knowing which factories opened, expanded, closed or filed for bankruptcy. Those developments matter, but they are only part of the picture.

An owner should also watch how other companies manage people, sell projects, develop dealer networks, communicate with developers, and present themselves online.

Management should be asking:

  • Are developers changing what they expect from modular manufacturers?
  • Are builders looking for components instead of complete modules?
  • Are customers responding differently to traditional sales methods?
  • Are competitors explaining their value more clearly?
  • Are new factories entering the market with lower overhead?
  • Are automation companies solving real production problems or simply selling impressive demonstrations?
  • Are lenders and investors becoming more cautious about offsite construction?
  • Are factories hiring different types of managers?
  • Are building-code, insurance or transportation changes creating new risks?
  • Are panelized, hybrid and mass-timber systems entering markets once dominated by volumetric modular construction?

You can’t answer any of these questions by watching production totals alone.

Some of the most valuable business lessons come from observing decisions other companies make.

A factory does not need to experience every mistake personally.

When another manufacturer expands too quickly, becomes dependent on one customer or purchases automation before preparing its workforce, there is something to learn. When a startup spends heavily on promotion but cannot create a dependable path from prototype to profitable production, established factories should pay attention.

The same is true when a company succeeds.

What did management do differently? Did it enter a carefully selected market rather than attempt to serve everyone? Did it improve engineering before expanding production? Did it build a strong dealer network? Did it hire experienced factory leadership instead of assuming technology could replace management?

The lesson is not necessarily to copy what another company did. Conditions vary too much for that. The value comes from examining the decision, understanding why it was made and asking whether something similar could affect your own business.

Factory owners sometimes treat marketing as something separate from operations. Production builds the product, while marketing makes the brochures, places advertisements and posts on social media.

That separation no longer makes sense.

Marketing influences what kinds of inquiries reach the factory, what customers expect, how the sales team explains the product, and whether the company attracts projects it can build profitably.

A factory website filled with attractive homes may generate attention but fail to answer the questions asked by builders, developers and investors. A company may promote customization without explaining that excessive customization disrupts engineering and production. Another may advertise speed without describing what must be completed before production begins.

Poor marketing can create poor prospects, unrealistic expectations and projects that do not fit the factory.

Keeping abreast of marketing means studying how the market is changing, what customers are asking and how competitors are presenting their capabilities. It also means being willing to look honestly at your own message.

If the factory has changed but its website has not, customers may be evaluating a company that no longer exists. If the company’s marketing promises more than its production system can deliver, the sales team may be filling the backlog with future problems.

Salespeople hear things that may never appear in a formal industry report.

They hear developers complain about financing. They learn which competitors are bidding aggressively, which projects are being delayed and which customers are beginning to consider panelization, pods or hybrid construction.

That information is valuable only if someone collects it and brings it into management discussions.

Communication must also flow in the other direction. Salespeople need to know what is happening in purchasing, engineering and production. They should understand which project types are profitable, which options cause disruption and how much production-ready capacity is actually available.

A company cannot keep abreast of the market if sales and production operate with different versions of reality.

Factories assign people to production, safety, quality control, estimating, engineering and purchasing. Yet many never assign anyone to monitor what is changing outside the company.

That responsibility does not require a full-time industry analyst. The owner, general manager, sales manager, or another employee with the curiosity and judgment to recognize meaningful developments could share it.

The assignment should be specific.

That person might review selected industry publications, newsletters, company announcements, conference reports, LinkedIn discussions and public financial information. He or she could follow a limited number of competitors, suppliers, technology companies, developers and industry organizations.

The objective is not to collect everything. It is to identify what might affect the company.

Once a week, that person could provide management with a short report containing:

  • What happened
  • Why it may matter
  • Whether it creates a risk or opportunity
  • Who should examine it further
  • What, if anything, the company should do next

A five-minute discussion during a management meeting may be enough to prevent an important development from going unnoticed.

The amount of available information can become overwhelming. An owner who tries to follow every article, podcast, webinar, press release and social-media post will eventually stop following any of them.

A better approach is to build a manageable information diet.

Choose a small number of credible sources covering offsite construction, housing, manufacturing, finance, technology, sales and management. Include sources from outside the modular industry because some of the most useful ideas may be emerging elsewhere.

Then separate information into three categories:

  • Immediate: Something that could affect a current customer, project, supplier or financial decision
  • Developing: A trend that deserves continued monitoring
  • Interesting: Worth knowing, but not important enough to require action

This distinction matters because every new idea can appear urgent when presented enthusiastically.

Most are not.

Artificial intelligence, robotics, mass timber, advanced panelization and new software platforms may influence the industry’s future. However, a factory should not chase every innovation it reads about. Management must decide whether the development addresses a real business problem and whether the company is prepared to use it.

Keeping informed should improve judgment, not replace it.

The greatest obstacle may not be a lack of information. It may be a management culture that no longer asks questions.

A company can become comfortable doing things the way they have always been done, especially when those methods produced success in the past. Employees learn that suggesting a different approach creates more trouble than remaining silent.

Over time, curiosity disappears.

A healthy management team should regularly ask what has changed, what customers are saying and what assumptions may no longer be valid. It should be willing to examine an unfamiliar idea without immediately embracing or dismissing it.

Curiosity does not mean abandoning experience. It means using experience to evaluate what comes next.

The experienced factory manager who understands why a proposed innovation will not work under real production conditions is providing valuable judgment. But the manager who rejects it simply because “we tried something like that 20 years ago” may be protecting the past rather than the company.

Reading more articles will not save a factory. Neither will attending every conference or subscribing to another newsletter.

Information becomes valuable only when it influences a decision.

That decision may be to investigate a market, revise a sales message, update the website, call a customer, train an employee, postpone an equipment purchase or begin preparing for a threat that has not yet reached the factory.

Sometimes the right decision is to do nothing.

But “we studied it and decided not to act” is very different from “we never saw it coming.”

An offsite factory should know what happened on its production line yesterday. It should also have some idea of what may be coming toward that line tomorrow.

I have spent years reading, listening, asking questions, and writing about this industry. That has not given me every answer. If anything, it has shown me how quickly yesterday’s certainty can become tomorrow’s outdated assumption.

Factory owners do not need to become industry reporters. They do need to develop the habit of looking beyond the problems immediately in front of them.

The companies most likely to endure will not necessarily be the ones with the newest factories, the largest backlogs or the most impressive technology. They may be the ones whose managers remain curious enough to notice change, disciplined enough to examine it and confident enough to act before everyone else recognizes that the industry has moved.

The Daily Plan That Could Keep an Offsite Factory Out of Crisis

Waiting until the last minute to address an offsite construction company’s financial problems is nothing new.

Owners and boards often sit back and watch conditions deteriorate because they are unsure what to do. Orders decline, cash becomes tight, suppliers begin calling, and the backlog that once looked reassuring turns out to contain projects that are delayed, underpriced or unlikely to reach production.

Eventually, management is told that its remaining choices are bankruptcy, liquidation or selling the company for enough money to pay the bills.

By then, the company is no longer choosing its future. Its lenders, creditors, customers and circumstances are choosing it.

What would be new is for an offsite company to study the problems that typically destroy otherwise profitable businesses and create an action plan for each one before any of them occur.

This is more than traditional strategic planning. It is a practical resilience system that management can review in approximately 15 minutes each day. It identifies developing threats, assigns responsibility and specifies what actions will be taken when conditions cross predetermined thresholds.

No plan can make a company completely bulletproof. However, an offsite factory that sees trouble developing early and has already decided how to respond can become much harder to surprise, weaken or destroy.

Most business planning begins with an optimistic question: How can we grow?

A resilience plan begins with a less comfortable question: What could bring us down?

The owner, board, and senior managers should identify the events most likely to threaten the company. They should not limit the discussion to dramatic disasters. Offsite companies are often weakened by ordinary problems that accumulate quietly over several months.

Those problems might include:

  • A 20 or 30 percent decline in new orders
  • The loss of a major builder, dealer or developer
  • A customer postponing a large project
  • Interest rates remaining high longer than expected
  • A lender reducing or declining to renew a credit line
  • A critical supplier failing or demanding different payment terms
  • Material costs increasing after project prices have been established
  • Warranty claims or rework consuming production capacity
  • A shortage of working capital during a period of apparent profitability
  • The sudden departure of a general manager, production manager or lead engineer
  • A transportation, crane or set-crew failure
  • A code, inspection or certification problem
  • A cyberattack or extended software outage
  • An accident that interrupts production
  • Excessive dependence on one market, customer or product
  • A backlog filled with projects that are not ready to be produced

Management should then ask three questions about every threat:

  1. What would be the earliest indication that this is beginning?
  2. At what point would we be required to take action?
  3. What actions could we prepare now rather than invent during the crisis?

This exercise should include people from sales, estimating, engineering, purchasing, production, finance and service. A problem that appears manageable from the executive office may look very different to the department that would have to solve it.

Identifying risks is useful, but it does not become a plan until each risk has a trigger, an owner and a predetermined response.

Suppose the factory normally maintains a confirmed backlog equal to 16 weeks of production. Management might establish three levels:

  • Green: More than 14 weeks of production-ready backlog
  • Yellow: Between 10 and 14 weeks
  • Red: Fewer than 10 weeks

A yellow condition might trigger a review of every pending proposal, additional calls to builders and developers, tighter control of overtime, and a delay in nonessential purchases.

A red condition might trigger reduced production hours, renegotiation of delivery schedules, more aggressive sales activity, a temporary hiring freeze, and immediate discussions with the lender.

The important point is that these decisions are made before fear, pride and confusion enter the discussion.

The same approach applies to cash. If unrestricted cash and available credit fall below a specified number of weeks of operating expenses, the company begins its yellow-level actions. If liquidity falls further, the red-level plan begins automatically.

This prevents management from spending several valuable weeks debating whether the situation is serious enough to require action.

Offsite companies often place too much confidence in the total dollar value of their backlog. A $40 million backlog sounds impressive, but it may not produce $40 million of work.

Some projects may be waiting for permits, financing, site preparation, engineering decisions or customer deposits. Others may have been priced before material or labor costs increased. A project expected to begin next month may remain on the backlog report for a year.

The daily resilience plan should divide backlog into at least three categories:

  • Production-ready: Approved, financed, engineered, deposited and scheduled
  • Conditional: Likely to proceed but still missing one or more requirements
  • Speculative: Reserved capacity or anticipated work without sufficient commitment

Only the production-ready backlog should be used to determine how many weeks of work the factory can safely expect.

Management should also track backlog profitability. A factory can be busy and still lose money if the work was poorly estimated or includes obligations that were never included in the price.

A growing backlog is not necessarily a sign of strength. A growing backlog of underpriced, delayed or unbuildable projects can become a liability.

The owner and management team do not need to spend hours every day reviewing dozens of reports. They need one page containing the few measurements that reveal whether the company is moving toward or away from trouble.

That dashboard might include:

  • Unrestricted cash and available credit
  • Cash runway expressed in weeks
  • Accounts receivable over 30, 60 and 90 days
  • Production-ready backlog in weeks
  • New orders received during the past 30 and 90 days
  • Proposal-to-order conversion rate
  • Gross margin on work sold and work currently in production
  • Deposits collected compared with deposits required
  • Schedule adherence
  • Labor hours per module, section, panel or square foot
  • Rework and warranty costs
  • Material shortages affecting scheduled production
  • Customer concentration
  • Supplier concentration
  • Banking covenant status
  • Safety or quality events capable of stopping production

Not every metric needs the same intensity of review every day. Most should be updated automatically or by the responsible department. The daily management review should concentrate on exceptions—measurements that have moved from green to yellow or from yellow to red.

If everything is green, the meeting may take five minutes. If something turns yellow, the responsible manager explains the reason and confirms that the planned response has begun.

The purpose is not to create another reporting burden. It is to make developing trouble impossible to ignore.

The daily meeting should be short, disciplined and held at the same time.

Participants might include the owner or general manager and the leaders of finance, sales, production, purchasing, and engineering. Smaller companies may have one person covering several of those responsibilities.

The meeting should answer five questions:

  1. Did any metric change status?
  2. What caused the change?
  3. Has the predetermined action begun?
  4. Who is responsible for the next step?
  5. When will the result be reported?

This is not the place for a lengthy discussion about how to solve every problem. If a yellow or red condition requires more attention, the appropriate people meet separately.

The resilience review protects management time by separating awareness from problem-solving. Everyone sees the warning, responsibility is assigned, and the people directly involved handle the details.

The daily review provides early warning, but the larger system needs two additional levels.

Once a week, management should spend approximately 45 minutes examining trends. A metric may remain green while gradually moving in the wrong direction. New orders, margins or productivity might decline slightly for six consecutive weeks without crossing a formal warning threshold.

The weekly review asks whether the business direction is changing.

Once a month, the owner and senior team should examine one or two larger scenarios. What would happen if orders declined 25 percent? What if the company’s largest customer failed? What if lumber, steel or transportation costs increased sharply? What if the lender reduced the credit line?

Management should calculate the financial and operational effect and confirm whether the existing response plan remains realistic.

The board should review the complete resilience plan quarterly. At least once a year, it should conduct a tabletop exercise in which one serious scenario is treated as though it has actually happened.

Probably not at the beginning.

Resilience should not be assigned to a new employee whom everyone else can conveniently ignore. Finance already produces cash information. Sales knows what is happening with orders and proposals. Operations tracks labor, schedules and production. Purchasing understands supplier risk.

The first requirement is not another salary. It is a system that connects the information the company already has.

Designate one senior person as the resilience coordinator. In a smaller company, that might be the owner, controller or general manager. In a larger organization, it might be the chief financial officer, chief operating officer or a director of business planning.

The coordinator does not own every risk. The coordinator ensures the dashboard is current, warning thresholds are respected, action plans are maintained, and assigned people report their progress.

A dedicated risk or resilience manager may eventually be justified if the company operates multiple plants, has a complex debt structure or is involved in unusually large projects. Most independent offsite factories should first prove that the system works with their existing leadership team.

A resilience plan should not be viewed only as a defensive tool. Studying potential problems often reveals ways to make the company more profitable.

Examining supplier risk may uncover alternative materials, better purchasing arrangements or opportunities to share inventory with another factory. Studying customer concentration may encourage the company to enter a new market before its largest customer leaves.

Reviewing labor productivity may identify stations where small equipment investments could reduce overtime. Examining cash requirements may lead to better deposit schedules, progress billing or contract language.

A scenario involving reduced orders might reveal that the factory could profitably produce components, panels, bathroom pods or assemblies for other builders. A discussion about financing risk might introduce the company to investors, lenders or development partners it had never previously considered.

The purpose is not to frighten the organization by imagining everything that could go wrong. It is to remove the element of surprise and discover options while the company still has the time, cash and credibility to use them.

The Board Must Be Willing to Act

The best dashboard in the world will not help if the owner or board refuses to respond to it.

Some owners will explain away a yellow warning because they believe a large order is about to arrive. Others will continue spending because they do not want employees or competitors to suspect that the company is concerned. A board may postpone difficult action because no individual director wants to be blamed for making an unpopular decision.

That is why the board should approve warning thresholds and responses in advance.

When the company is healthy, management can calmly decide what will happen if cash, backlog, margins or productivity reach dangerous levels. When the trigger occurs, the discussion is no longer about whether somebody is overreacting. The company is carrying out a plan everyone previously accepted.

The system only works when yellow means action and red means immediate action.

Gary’s Observation

Offsite construction companies rarely collapse because one bad thing happens on a Tuesday morning. They usually decline gradually while everyone waits for sales to improve, financing to arrive, a delayed project to begin or the next big customer to save them.

By the time the owner admits that something must be done, many of the best options have disappeared.

The new idea is not another complicated strategic plan that sits in a binder until the annual board meeting. It is a living resilience plan: one page reviewed daily, a short list of meaningful metrics, warning levels you cannot ignore, and actions decided before the crisis begins.

It will not make an offsite company invincible. It will do something almost as valuable.

It will give the company time to act while it still has choices.

What Could Possibly Go Wrong When Smart People Decide to Build a Modular Factory?

I’m still amazed by a group of highly intelligent people’s ability to collectively make an incredibly stupid decision.

Individually, these people may be successful entrepreneurs, engineers, architects, developers, attorneys, technology executives, or investors. They have impressive résumés, successful careers, and enough business experience to know that starting any manufacturing company requires customers, capital, management, research, and a solid plan.

Then somebody mentions affordable housing and modular construction, and much of that accumulated business wisdom seems to leave the room.

Someone says the country desperately needs more housing for people who can’t afford what is currently being built. Everyone agrees because it’s obviously true. Someone else mentions homelessness, workforce housing, teachers, nurses, first-time buyers, or families living near the poverty line, and soon the group is discussing how traditional construction simply isn’t producing enough affordable homes.

Then someone remembers that he knows someone who works at a modular factory. Maybe it’s a former employee, a cousin, a business associate, or the brother-in-law of someone he met at a conference. It really doesn’t matter because the word “factory” has entered the conversation.

Someone says, “Why don’t we build the homes in a factory?” Another person points out that factories can build things faster. Someone else says automation should make them cheaper. Another starts talking about robotics, and before anyone has bothered to ask what an affordable home actually needs to cost, the conversation has moved from discussing America’s housing shortage to planning a modular factory.

Ten minutes ago, they wanted to help people find affordable housing. Now they want to become manufacturers.

The excitement builds quickly because modular construction looks wonderfully logical from the outside. Put workers under a roof, bring materials to them instead of sending workers to job sites, use repetitive processes, install modern equipment, reduce weather delays, and send completed modules to waiting foundations. What could possibly go wrong?

Someone opens a laptop and finds a video showing modules gliding smoothly through a factory. Another person Googles industrial buildings. Someone begins estimating how many homes could be produced every week. Before long, six highly intelligent people who have never designed, engineered, permitted, financed, manufactured, transported, set, finished, warranted, or sold a modular home have mentally built a factory that can produce 1,000 affordable homes a year.

They haven’t identified enough customers to keep the factory busy. They haven’t secured land for those homes, investigated zoning, studied transportation distances, talked with local officials, priced foundations and utilities, found set crews, or determined who will provide construction financing. They also haven’t figured out what happens when completed modules are sitting in the factory yard because the jobsites aren’t ready.

Most importantly, nobody has asked the question that could ruin the entire meeting: Affordable to whom, and at what finished price?

Why spoil a perfectly good startup with details?

Once the imaginary factory is running beautifully inside everyone’s head, the group needs money. That means preparing a pitch deck explaining that America has a housing shortage, which somehow becomes the market research supporting the new factory.

The presentation will probably include photographs of housing problems, charts showing rising home prices, statistics about millions of missing homes, and attractive renderings of a futuristic modular factory that doesn’t exist. Somewhere in the presentation will be artificial intelligence, robotics, automation, sustainability, digital twins, advanced manufacturing, or preferably all of them.

By slide 17, homes are flying out the factory door. By slide 22, the company is profitable. By slide 28, the founders are discussing factories number two and three. There may even be a map showing future factories strategically located across the United States.

The only thing still missing is customers.

Fortunately, our group eventually finds another group of highly intelligent people called investors. The entrepreneurs believe the investors understand modular construction, while the investors assume the entrepreneurs do. Neither group wants to be the one asking the uncomfortable questions while everyone else talks about changing the world.

Now two groups of highly intelligent people who may know almost nothing about modular manufacturing are officially off to the races.

Eventually, somebody around the table says something genuinely intelligent: maybe we should talk with someone who actually knows the modular industry. That is an excellent idea, but it introduces another problem because consultants in our industry tend to come in three very different flavors.

The first type is the Enthusiastic Consultant. He loves the idea almost as much as the founders do. A new modular factory producing affordable housing with automation and innovative technology sounds exciting, and he immediately begins helping them figure out how to make it happen.

Instead of asking whether the factory should exist, he starts helping design it. He researches equipment, discusses production lines, recommends software, talks about factory layouts, and begins introducing suppliers. Pretty soon everyone is working extremely hard solving problems for a business nobody has proven should exist.

Then we have the second type, whom I’ll call the Cash Register Consultant. This consultant has enough industry experience to recognize exactly what’s happening. He knows the production estimates are optimistic, the startup schedule is fantasy, working capital is probably inadequate, and the sales forecast is mostly wishful thinking.

He also recognizes something else: these people have money.

So why interrupt them? He’ll write reports, attend meetings, recommend equipment, introduce vendors, develop schedules, and revise those schedules when they don’t work. When the original budget proves inadequate, he’ll help prepare another one. If the investors eventually start asking what happened to all their money, he may even recommend another study to determine why.

Some consultants help startups build successful factories. Others simply help startups spend their money more professionally.

The third consultant can become extremely annoying very quickly because instead of congratulating everyone on their brilliant idea, he starts asking questions. He wants to know exactly who the customer is, what that customer can afford, who owns the land, who will develop it, and what the completed home will cost after transportation, foundation, crane, installation, utilities, permits, site work, financing, sales costs, and builder margin are included.

He wants to know how many homes customers have actually committed to purchase and what happens if first-year production reaches only half the volume shown in the pitch deck. He asks about working capital, factory management, sales, warranty service, transportation, set crews, local zoning, engineering approvals, labor availability, material purchasing, and what happens when finished modules start accumulating in the yard.

Then he asks what may be the most irritating question of the entire meeting: Why do you need to build a factory at all?

Suddenly, the excitement level drops. The experienced consultant, invited for his or her superior industry knowledge, starts to sound negative. He doesn’t understand the vision. He’s thinking like the old modular industry. He isn’t entrepreneurial enough, and he clearly doesn’t understand how technology will change everything.

Or maybe he’s the first person in the room who is actually trying to save their money.

Entrepreneurs sometimes struggle to accept this. A good consultant isn’t hired to tell you how brilliant your idea is or how much the industry needs another innovative factory. Plenty of people are willing to provide encouragement for free.

An experienced consultant should be willing to tell you that your proposed factory is too large, your market is too small, your capital is inadequate, your timeline is unrealistic, your management team lacks manufacturing experience, or your customers don’t exist in sufficient numbers. More importantly, that consultant should be willing to tell you those things before you buy a building, order equipment, hire employees, and burn through millions of dollars.

He may suggest starting with 25 homes instead of building a factory capable of producing 1,000. He might recommend contracting production with an existing manufacturer, proving the market before buying a single saw, becoming a developer first and a manufacturer later, or partnering with a factory that already knows how to build what you’re trying to sell.

He might even study everything you’ve assembled, listen to the grand vision, review the projections, push the business plan back across the table, and politely say, “No, thanks.”

That could be the most valuable consulting advice the group ever receives.

None of this means these entrepreneurs or investors are actually stupid. Quite the opposite. The problem is that intelligence creates confidence, and success in one industry can convince people that it will automatically transfer to another. Sometimes it does, but modular construction has humbled plenty of smart, successful people who thought it would be easier than it turned out to be.

From the outside, modular construction appears deceptively simple. Put construction workers inside a building, establish an assembly line, buy better equipment, introduce automation, build homes faster than site builders, and attack the affordable housing shortage. It sounds so logical that the biggest mystery becomes why the existing modular industry hasn’t already done it.

The answer is that a modular factory isn’t simply a manufacturing operation. It sits in the middle of manufacturing, construction, transportation, real estate development, financing, zoning, building codes, engineering, labor, supply chains, sales, installation, warranty service, and local politics. Success doesn’t require making one of those systems work exceptionally well. It requires making them all work together at the same time.

That’s where highly intelligent people can become highly intelligent stupid people surprisingly quickly.

I love entrepreneurs and people willing to challenge an industry and try something new. Offsite construction desperately needs fresh ideas, new technology, new capital, better processes, and people willing to question why we’ve been doing certain things the same way for decades.

What the industry doesn’t need is another $30 million factory built around a PowerPoint presentation, a national housing-shortage statistic, and six smart people convincing one another that because affordable housing is desperately needed, buyers will automatically appear when the first module rolls out the door.

Before deciding to build a modular factory, find someone who knows enough about this industry to try to talk you out of it. Ask that person to attack your assumptions, your market, your numbers, your production estimates, your management plan, your working capital, and especially your definition of “affordable.” Don’t hire that person to validate your dream. Hire them to find out whether the dream has any chance of surviving reality.

If the idea survives that conversation, you may actually have something worth pursuing. And if the consultant looks across the table after hearing the entire plan and says, “No, thanks,” don’t immediately start searching for another consultant who will say yes.

You may have just received the best—and cheapest—advice of your entire startup.

What Does Cavco Know That the Rest of the Housing Industry Doesn’t?

Every so often, a factory announcement comes along that makes me stop and read it twice. Cavco Industries’ decision to build a 616,000-square-foot manufactured and modular home factory in El Mirage, Arizona, was one of those announcements.

This isn’t an expansion added to the back of an existing plant, nor is it an abandoned industrial building being converted into home production. Cavco is building a new, fully temperature-controlled manufacturing campus from the ground up on approximately 39 acres in the western Phoenix metropolitan area. The company broke ground earlier this year; the walls are now going up, and production is scheduled to begin by mid-2027.

When a company with Cavco’s experience commits to a factory this large, the interesting question isn’t simply how many homes it expects to build. The more important question is what Cavco sees coming in the Southwest that convinced its leadership and board this project makes sense.

Cavco’s public announcement says the El Mirage facility will produce both HUD-code manufactured homes and modular single-family homes for Arizona and surrounding states. It will begin with one production line, but the building is being designed so the company can add a second line later for what it calls “modest additional capital.”

That is a carefully calculated way to approach expansion. Cavco can bring the first line online, train the workforce, refine material flow, test market demand, and correct problems before committing to full production. If demand develops as expected, much of the second-line infrastructure will already be in place.

The planning documents submitted to the City of El Mirage reveal that this is more than a giant empty building with a conventional production line running through it. The proposed campus includes a 504,000-square-foot main manufacturing building, four material-storage structures, covered storage areas, two chassis shops, administrative offices, employee facilities, and outdoor staging for finished homes awaiting transportation.

Those components total approximately 640,350 square feet, somewhat more than the 616,000 square feet in Cavco’s public announcement. That difference may reflect a design revision or simply how covered storage and accessory buildings are counted, but either number makes this one of the most significant new factory-built housing projects in the country.

The factory plans describe two mirrored production lines sharing a central cabinet shop, mill shop, and countertop fabrication area. Cavco also intends to use CNC equipment, welding fixtures, overhead cranes, paint booths, centralized compressed air, utility trenches, and dust and fume collection systems. Onsite chassis fabrication and component production should give the company greater control over quality, scheduling, inventory, and costs.

This sounds less like Cavco is building a larger version of yesterday’s manufactured home factory and more like it is trying to establish a new production model for tomorrow.

Cavco expects to employ approximately 228 people when the plant opens. Employment could eventually grow to 455, although the planning documents indicate about 372 employees would be onsite when both lines are operating at the expected level.

That is a substantial workforce to recruit, train, and retain in one of the country’s fastest-growing metropolitan regions. The factory may be automated in important areas, but homes will still require skilled people who understand framing, electrical work, plumbing, roofing, cabinetry, finishing, quality control, material handling, engineering, and production management.

The labor question may prove almost as important as the housing demand question. A state-of-the-art building does not automatically create a state-of-the-art operation, especially during the first year when equipment, processes, suppliers, supervisors, and new employees are all learning to work together.

Then there is downstream capacity, which rarely gets as much attention as the factory. More homes leaving El Mirage will require more retailers, developers, land, financing, permits, transporters, set crews, foundations, utility connections, and local jurisdictions willing to accept manufactured and modular housing.

Factories can increase production much faster than communities can approve subdivisions or install infrastructure. Cavco may be able to build hundreds or even thousands of additional homes, but those homes still need somewhere to go when they reach the end of the production line.

The Southwest continues to struggle with housing affordability, population growth, land costs, and a shortage of attainable entry-level homes. Arizona, Nevada, New Mexico, California, Colorado, and parts of Texas all present possible opportunities, but they are not one uniform market.

Each state brings its own transportation distances, zoning restrictions, energy requirements, labor conditions, financing challenges, and attitudes toward factory-built housing. A home that works competitively in rural Arizona may face an entirely different set of costs and approvals in suburban California.

Cavco has said the plant will produce both manufactured and modular single-family homes, which gives it more flexibility than a factory committed to one product category. The HUD-code side can serve retailers, land-lease communities, individual homebuyers, and developers. The modular side could potentially serve subdivisions, build-to-rent projects, workforce housing, infill lots, and other developments requiring state or locally approved construction.

What Cavco has not publicly disclosed may be more interesting than what it has announced. We do not yet know the expected number of floors per day, the intended product mix, the amount of automation, the investment required, or whether production will supplement or eventually replace capacity at older Cavco facilities in the region.

We also do not know whether large developers, communities, retailers, or institutional buyers are already helping support the business case. Companies rarely build a factory of this size based solely on the hope that individual buyers will appear after the doors open.

Cavco reported record annual production of 34,745 factory-built modules in its latest fiscal year, a 7.1% increase over the previous year. That suggests the company is expanding from a position of operating strength rather than trying to rescue a declining business. Still, adding capacity is one thing; feeding it with profitable, repeatable orders is another.

The El Mirage factory could become an important test for more than Cavco. It could show whether the manufactured and modular housing industries can finally connect modern production capacity with the land, financing, zoning, transportation, installation, and development systems needed to deliver homes at scale.

For years, we have heard that offsite construction is the answer to America’s housing shortage. I believe it can be part of the answer, but the industry sometimes talks as if building more factories automatically produces more affordable housing.

It doesn’t. A factory produces the home, but affordability depends on the entire chain from the first engineering drawing to the day the homeowner gets the keys.

If land prices, impact fees, site work, transportation, financing, zoning delays, utility costs, and installation expenses keep climbing, even an extremely efficient factory will struggle to deliver the affordability promised in the press release. Cavco’s challenge will be to make the new plant more than a production achievement. It must become part of a coordinated housing delivery system.

The size of Cavco’s El Mirage project tells me that this is not a casual expansion. A 616,000-square-foot facility with room for two production lines, onsite chassis fabrication, central component shops, advanced equipment, and nearly 500 potential employees represents a long-term wager on factory-built housing in the Southwest.

Cavco may be anticipating stronger demand from developers, changing zoning attitudes, wider acceptance of HUD-code homes, growth in modular subdivisions, or financing programs that have not yet reached the broader market. It may also believe many older factories simply will not meet future expectations for production efficiency, employee working conditions, quality control, and product flexibility.

The factory itself is impressive, but its real importance will not be measured in square feet. It will be measured by how many homes it can produce profitably, how quickly those homes reach prepared sites, and whether families can actually afford the final delivered price.

Maybe Cavco simply believes the Southwest needs a lot more homes. Or perhaps it knows something about the next stage of factory-built housing that the rest of us are only beginning to see.

Why Do Offsite Companies Avoid Hiring Experienced Advisors?

I have often wondered why offsite construction companies hire consultants, advisors, and marketers who have little or no experience in offsite construction, yet hesitate when someone with decades of industry experience walks through the door.

It is one of the strangest contradictions in our industry. Owners and executives will tell anyone who listens that offsite construction is different from conventional construction. They will explain that designing, approving, manufacturing, transporting, setting, and finishing a building requires an entirely different way of thinking. Then, when they need help, some of those same leaders hire someone who has never worked inside that process.

There is nothing inherently wrong with bringing in an outsider. Fresh thinking can be valuable. Specialists in finance, technology, marketing, human resources, and organizational development can introduce ideas that an industry veteran might overlook. But fresh eyes and uninformed eyes are not the same thing.

An advisor who does not understand offsite construction may offer advice that sounds excellent in a conference room but falls apart the moment it reaches engineering, purchasing, or the production floor.

One reason experienced offsite professionals may be avoided is that they recognize problems quickly. They have seen factories struggle with poor estimating, engineering backlogs, inadequate working capital, unprofitable projects, labor shortages, dealer conflicts, transportation problems, delayed sets, warranty claims, and customers who change specifications after production begins.

They know that a full production schedule does not necessarily mean the company is profitable. They understand that increasing sales can make a cash-flow problem worse. They also know that a factory can look busy right up until the day it runs out of money.

That experience leads them to ask questions owners may not want to answer.

Can the factory produce what the sales team is promising? Is the company making money on every module, or simply generating revenue? Are deposits being used to build the customer’s project or to pay yesterday’s overdue bills? Who controls change orders? How long does a project remain in engineering before it reaches production? What happens when manufacturing is complete but the site is not ready?

Those questions are not nearly as exciting as a presentation about rapid growth, artificial intelligence, lead generation, cultural transformation, or brand awareness. They are, however, the questions that can keep a company alive.

Consultants and marketers from outside the industry sometimes arrive with a message leadership wants to hear. They promise more leads, a stronger brand, better systems, rapid expansion, or entry into new markets. Their presentation may be polished, their terminology impressive, and their projections encouraging.

The experienced offsite advisor is more likely to say, “Before we increase sales, let’s determine whether your engineering department and factory can handle the work.”

That response can sound negative to an owner who wants growth. In reality, it may be the most optimistic advice anyone could give. Growth without operational readiness does not solve problems. It multiplies them.

Marketing is a good example. A marketing firm may produce beautiful materials and generate qualified prospects, but what happens if the sales team makes promises the factory cannot keep? What happens if the company markets a product that has not been fully engineered, approved, priced, or tested in production?

More leads will not correct an operational weakness. They may simply expose it faster.

There may also be a psychological reason experienced people are sometimes kept at a distance. It is easier to explain a factory’s problems to someone who has never managed one.

An inexperienced consultant may accept the explanation that the company only needs more sales. Someone who has operated in the industry may discover that the real problem is estimating, scheduling, purchasing, productivity, project selection, or cash management.

The outsider hears the story leadership tells. The experienced advisor compares that story with what is happening inside the business.

That does not always make the experienced advisor popular. He or she may challenge a favorite project, question an unrealistic forecast, or point out that the company is accepting work it cannot profitably produce. They may also recognize that a problem blamed on employees actually began with ownership or senior management.

Experience reduces the owner’s ability to control the narrative, and that can be uncomfortable.

Cost is undoubtedly another factor. Experienced professionals may charge more than someone trying to enter the offsite market. But the larger difference may be their willingness to establish boundaries.

Someone who understands the industry is more likely to refuse an assignment with unrealistic expectations. They may decline to endorse a questionable business plan, promise an impossible turnaround, or support a factory startup that has not demonstrated sufficient demand or working capital.

Less-experienced consultants may be more willing to accept the owner’s assumptions because they do not yet recognize the warning signs. They can produce the requested report, campaign, or strategy without realizing that the underlying business is not ready to execute it.

The lowest consulting fee can become extremely expensive when the recommendations lead a company in the wrong direction.

This is not an argument that every advisor must have spent 30 years managing a modular factory. Outside expertise has an important place in offsite construction. Our industry needs new technology, better financial controls, stronger marketing, improved recruitment, modern software, and ideas borrowed from other forms of manufacturing.

But outside specialists should usually be paired with people who understand how offsite construction actually works. A financial consultant should know why cash moves differently through a factory-built project. A marketer should understand the relationship between sales volume and production capacity. A technology advisor should recognize that software cannot repair a broken operating process by itself.

The outside specialist may know the tool. The offsite veteran knows where—and whether—it can be used.

Offsite construction companies do not have to choose between fresh ideas and industry experience. The strongest advisory team can provide both. Problems arise when unfamiliarity is mistaken for objectivity and polished presentations are valued more highly than practical knowledge.

Offsite companies rarely get into serious trouble because nobody offered them an impressive new idea. They get into trouble because nobody in the room had enough industry experience—or enough independence—to challenge an unrealistic one.

Schedule a FREE Video Conference

Hiring an experienced offsite advisor may make an owner uncomfortable. But sometimes that discomfort is exactly what the company is paying for.

..

..

..

..

..